Precision Industrial Valves for Critical Applications
Engineered for reliability, durability, and extreme performance. We manufacture high-grade ball, needle, gate, and check valves designed for Oil & Gas, Chemical, and Water Treatment industries.
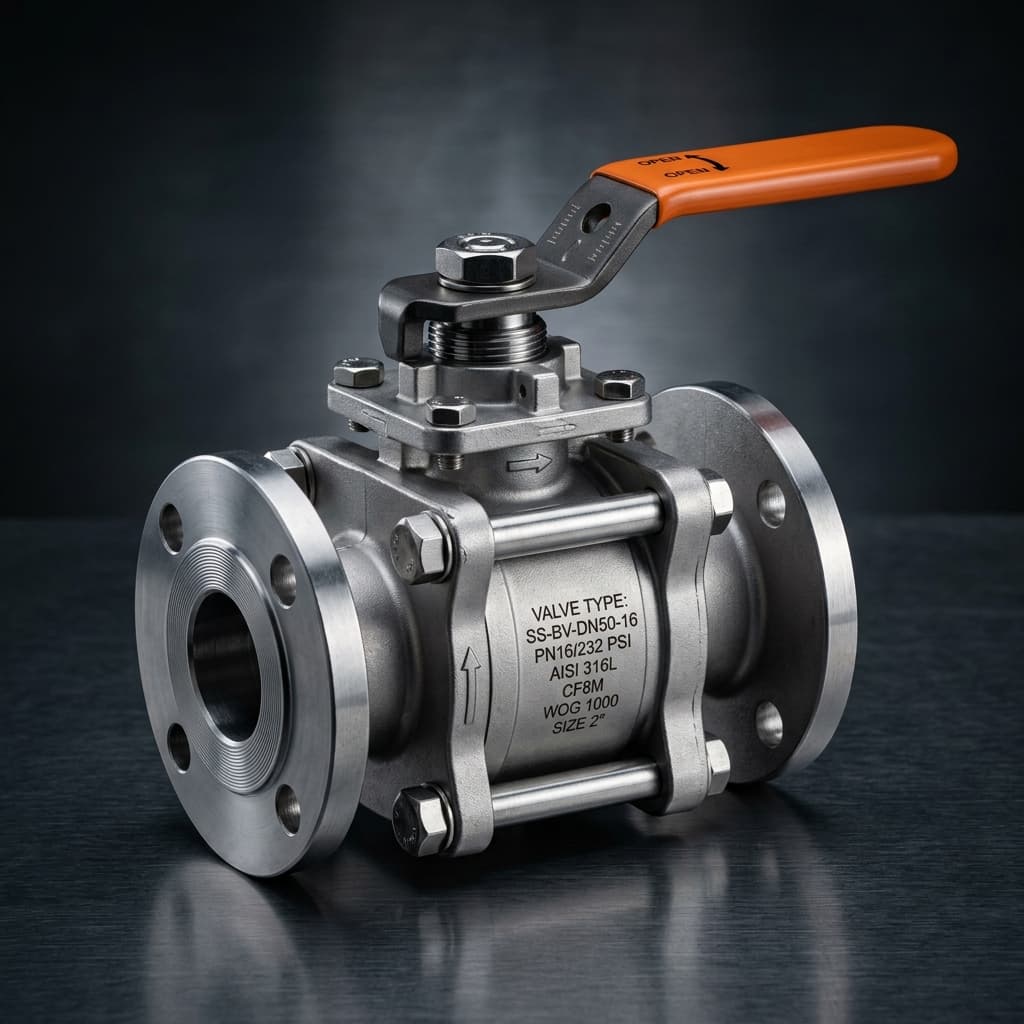
3-Piece High Pressure Flanged Ball Valve
Designed for high pressure chemical and steam applications with reinforced PTFE seat and blow-out proof stem.
Engineered Valve Categories
Browse our comprehensive selection of high-performance valves designed for specific pressure, temperature, and fluid requirements.
Featured Industrial Valves
Discover our most requested, field-tested valves engineered for critical processing pipelines.
Industries We Serve
Providing engineered fluid control products tailored for demanding operating environments.
Oil & Gas
High-pressure, fire-safe, and sour gas compliant valves built for upstream drilling and downstream refining.
Chemical Processing
Corrosion-resistant Hastelloy, Monel, and Duplex alloys for handling aggressive acids and solvents.
Water & Wastewater
Reliable flow control and backflow prevention for municipal water networks and desalination facilities.
Power Generation
Severe service steam isolation, blowdown, and feed-water valves certified for power plant boilers.
100% Pressure Tested
Every valve undergoes hydro & pneumatic pressure testing before shipment.
Fast Quote Turnaround
Receive technical specs and formal pricing quotes within 24 business hours.
Specialty Alloy Manufacturing
Available in Stainless Steel 316, Monel, Hastelloy, and Titanium.
Global Shipping
Worldwide logistics support with export packaging and customs compliance.
Ready to Upgrade Your Industrial Fluid Control Systems?
Submit your inquiry online or speak with our valve applications engineers for customized specifications and fast quote delivery.